Powerflo
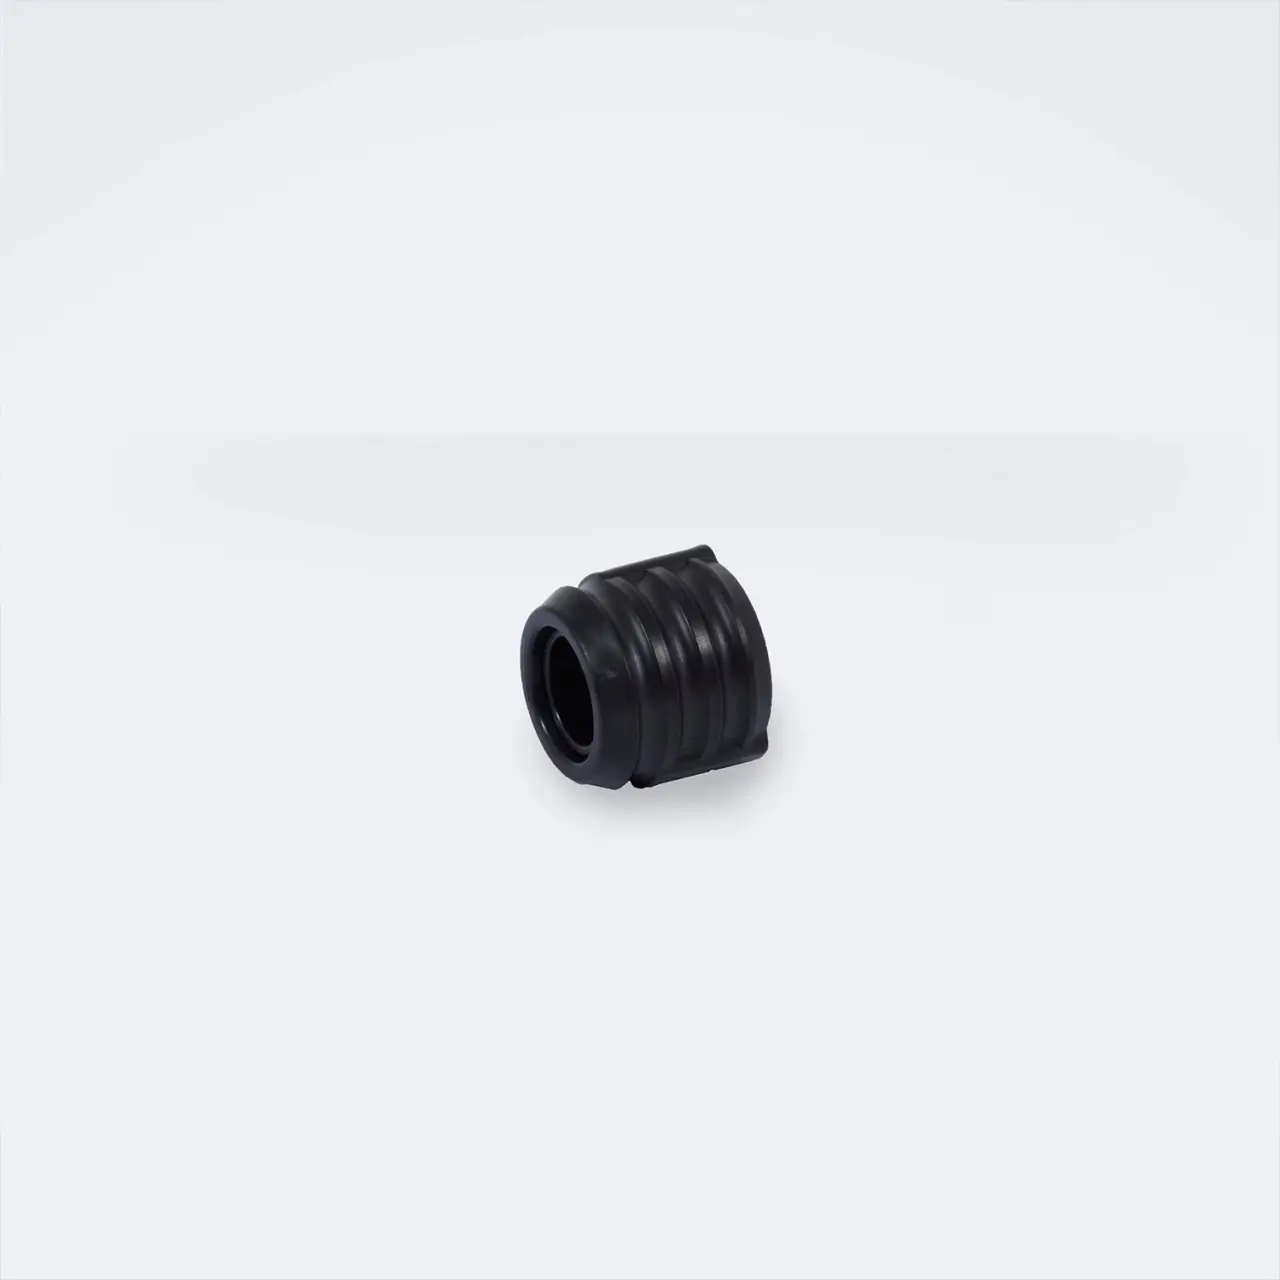
PF160
Quick Release Coupling
Quick Release Coupling to Fit Foamer Spraygun is a practical choice for everyday workplace requirements.
NZ owned & operated · ISO 9001 certified · Smarter Cleaning Systems since 1985
Industry solutions
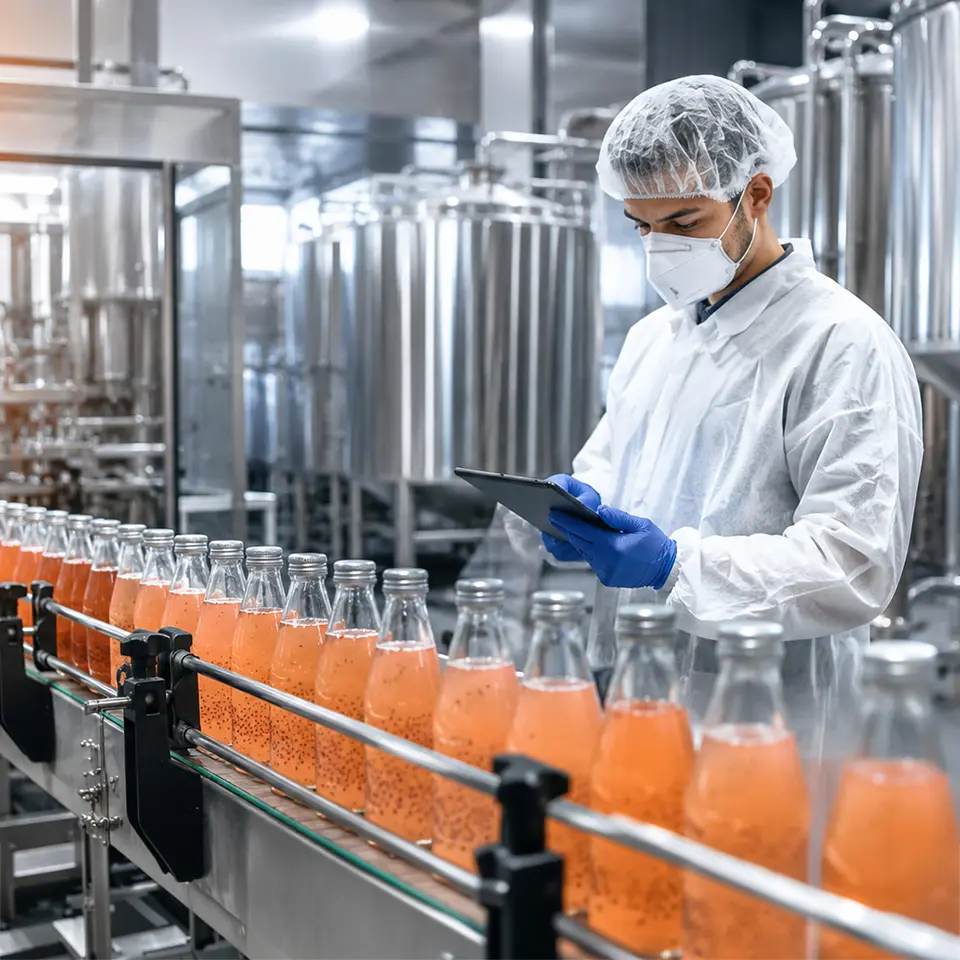
Food and beverage manufacturers face the toughest hygiene standards in New Zealand. MPI, BRC, Halal and customer audits all demand documented, repeatable cleaning. We supply complete systems: colour-coded tools, food-safe chemicals, contamination control and the visual management to hold it all together.
Audit compliance
MPI, BRC and customer audits demand documented hygiene systems with full traceability.
Allergen segregation
Colour-coded zoning prevents cross-contact between allergen and non-allergen areas.
Foreign object risk
Metal-detectable tools and shadow boards eliminate lost-equipment product recalls.
How we help
Start with the outcome you need. Each solution brings the right brands, tools and documentation together.
Food-safe detergents, sanitisers and skincare products selected for your surfaces, processes and hygiene risks, supported by clear technical documentation.
Explore cleaning & disinfection chemicalsCustom shadow boards, KPI boards and 5S systems that make zoning, tool control and cleaning standards visible at the point of use.
Explore visual managementReview chemical use, labour, water, equipment, tool life and downtime to identify practical savings without weakening hygiene performance.
Explore solutionChemclean delivers hard-working cleaning and sanitising chemicals for New Zealand’s agriculture and food processing industries.
ExplorePowerflo designs and supplies complete chemical delivery, application and washdown systems for demanding hygiene environments.
ExploreFlexible service solutions that work around your production schedule, reducing disruption and keeping downtime to a minimum.
ExploreDesigned around your site, processes and people to improve organisation, visibility, safety and compliance.
Explore
Quick Release Coupling to Fit Foamer Spraygun is a practical choice for everyday workplace requirements.
Nilium (Cucumber Melon) is a practical choice for everyday workplace requirements.
Available in 3 sizes, 2 bristles and 5 colours
These are designed for cleaning vehicles, buildings, vats and tanks etc.
Made of stainless steel. A practical choice for everyday workplace requirements. Designed for reliable professional use.
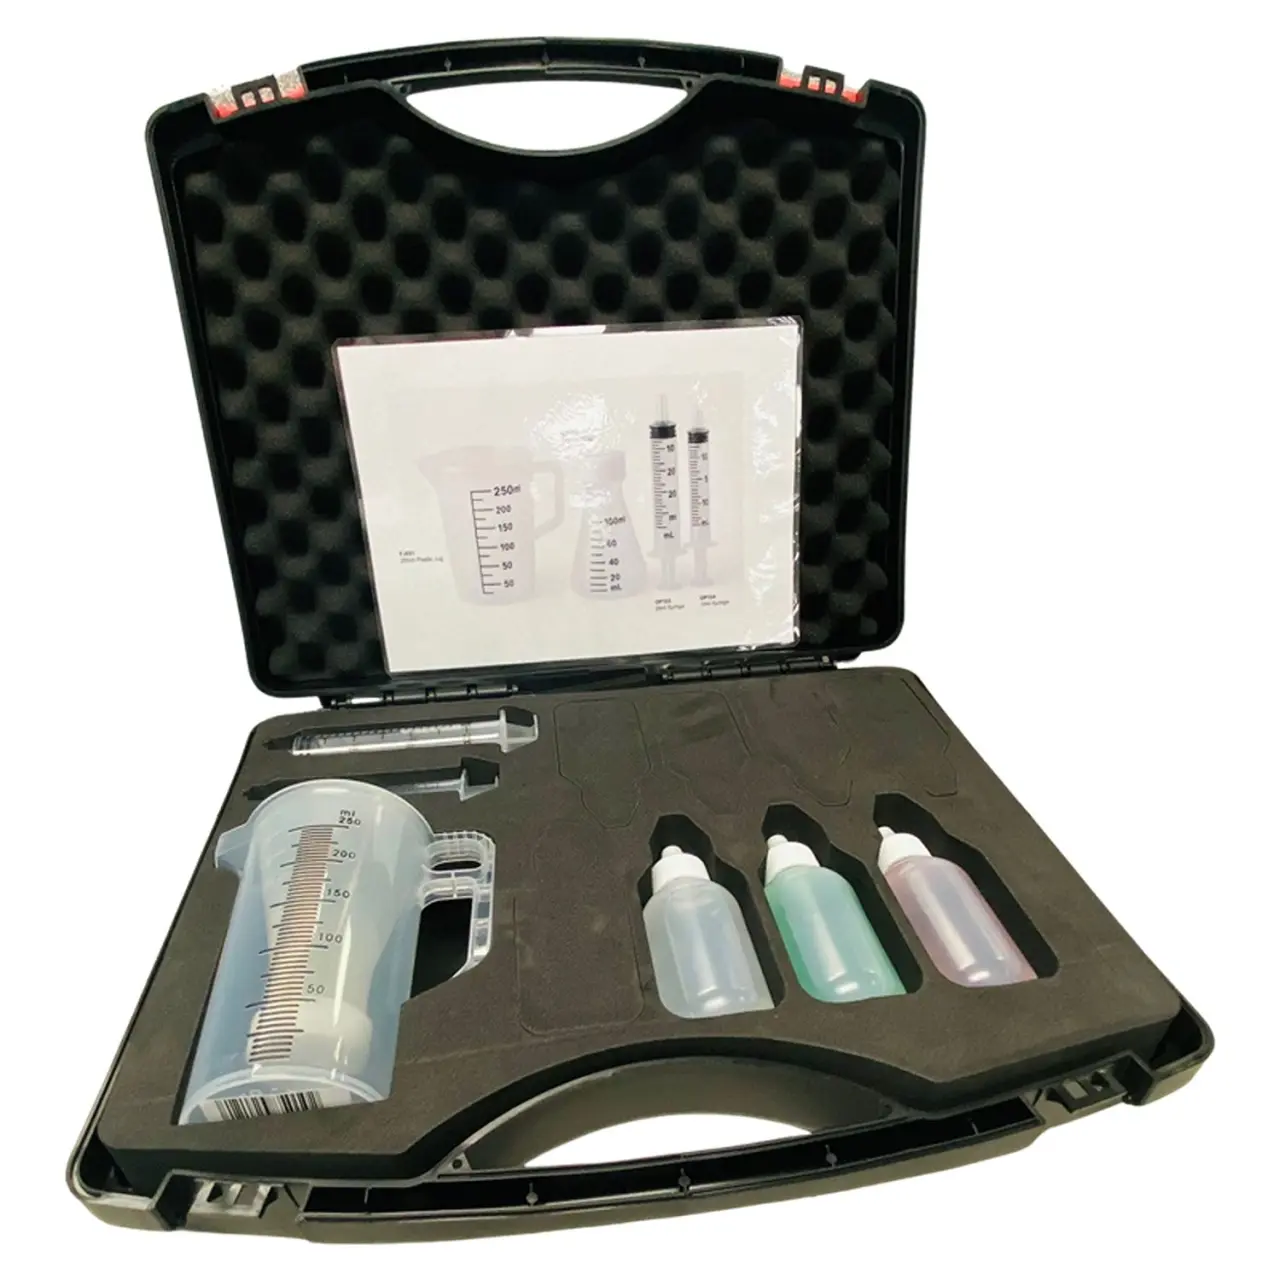
Ecofoam Titration Kit is designed for reliable professional use in hygiene verification. Precision You Can Trust.
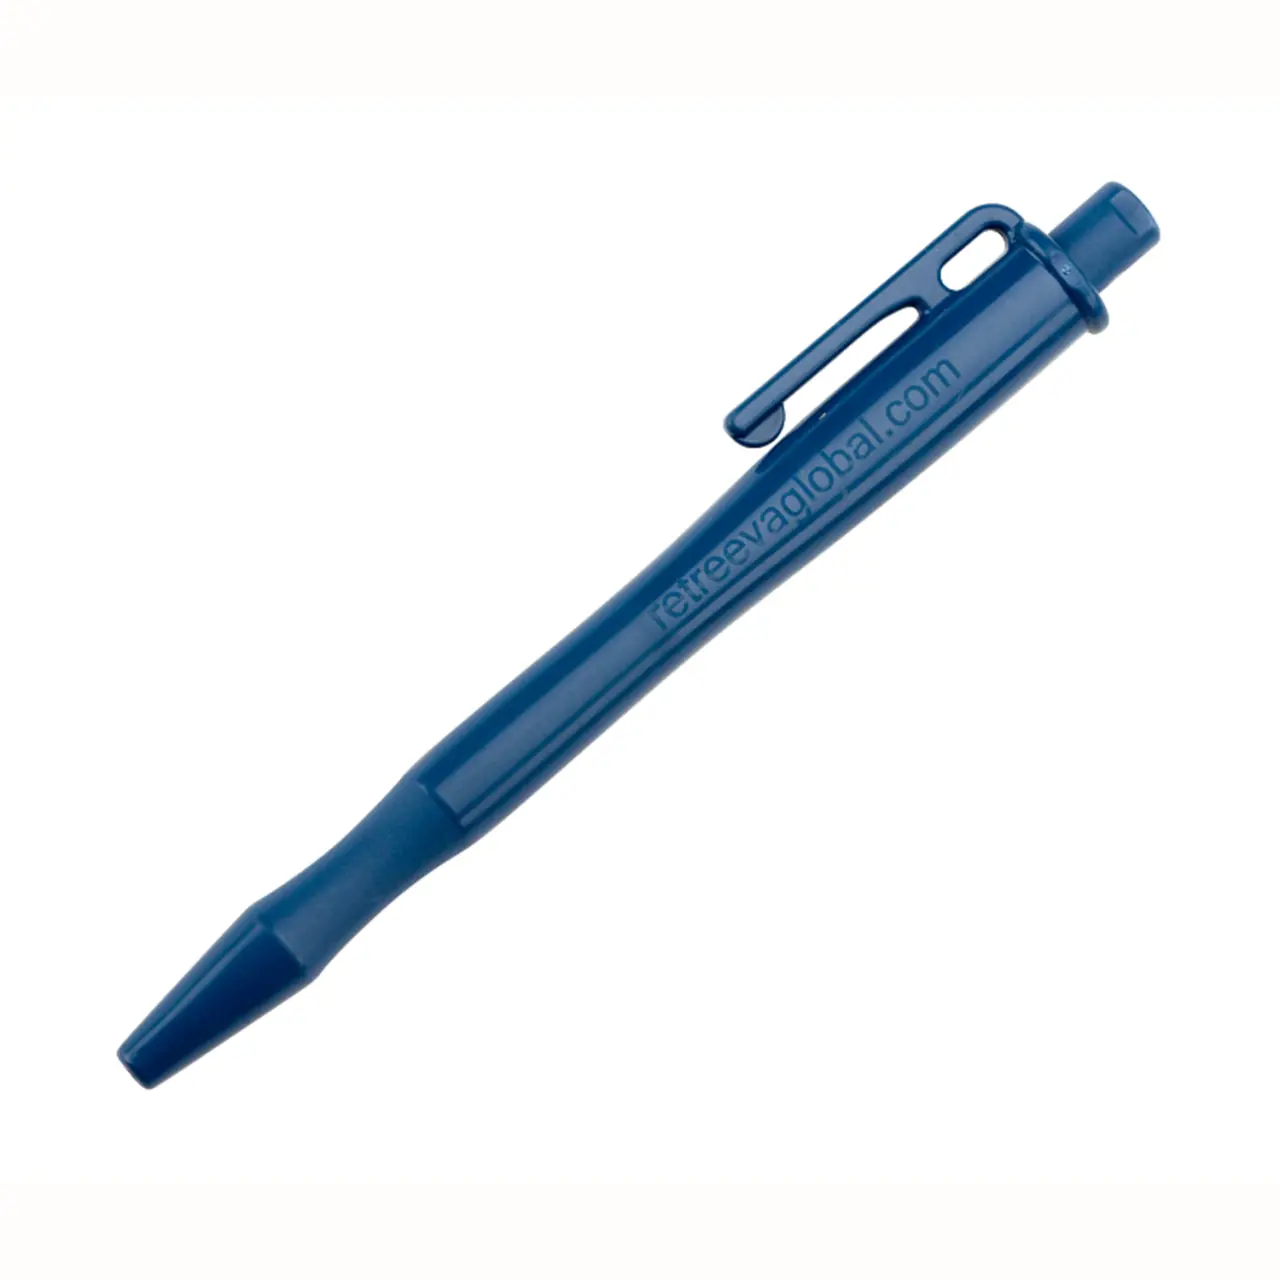
Available in 4 colours
Retreeva Detectable Retractable Pen is part of the Retreeva detectable writing range for food (25 per box).
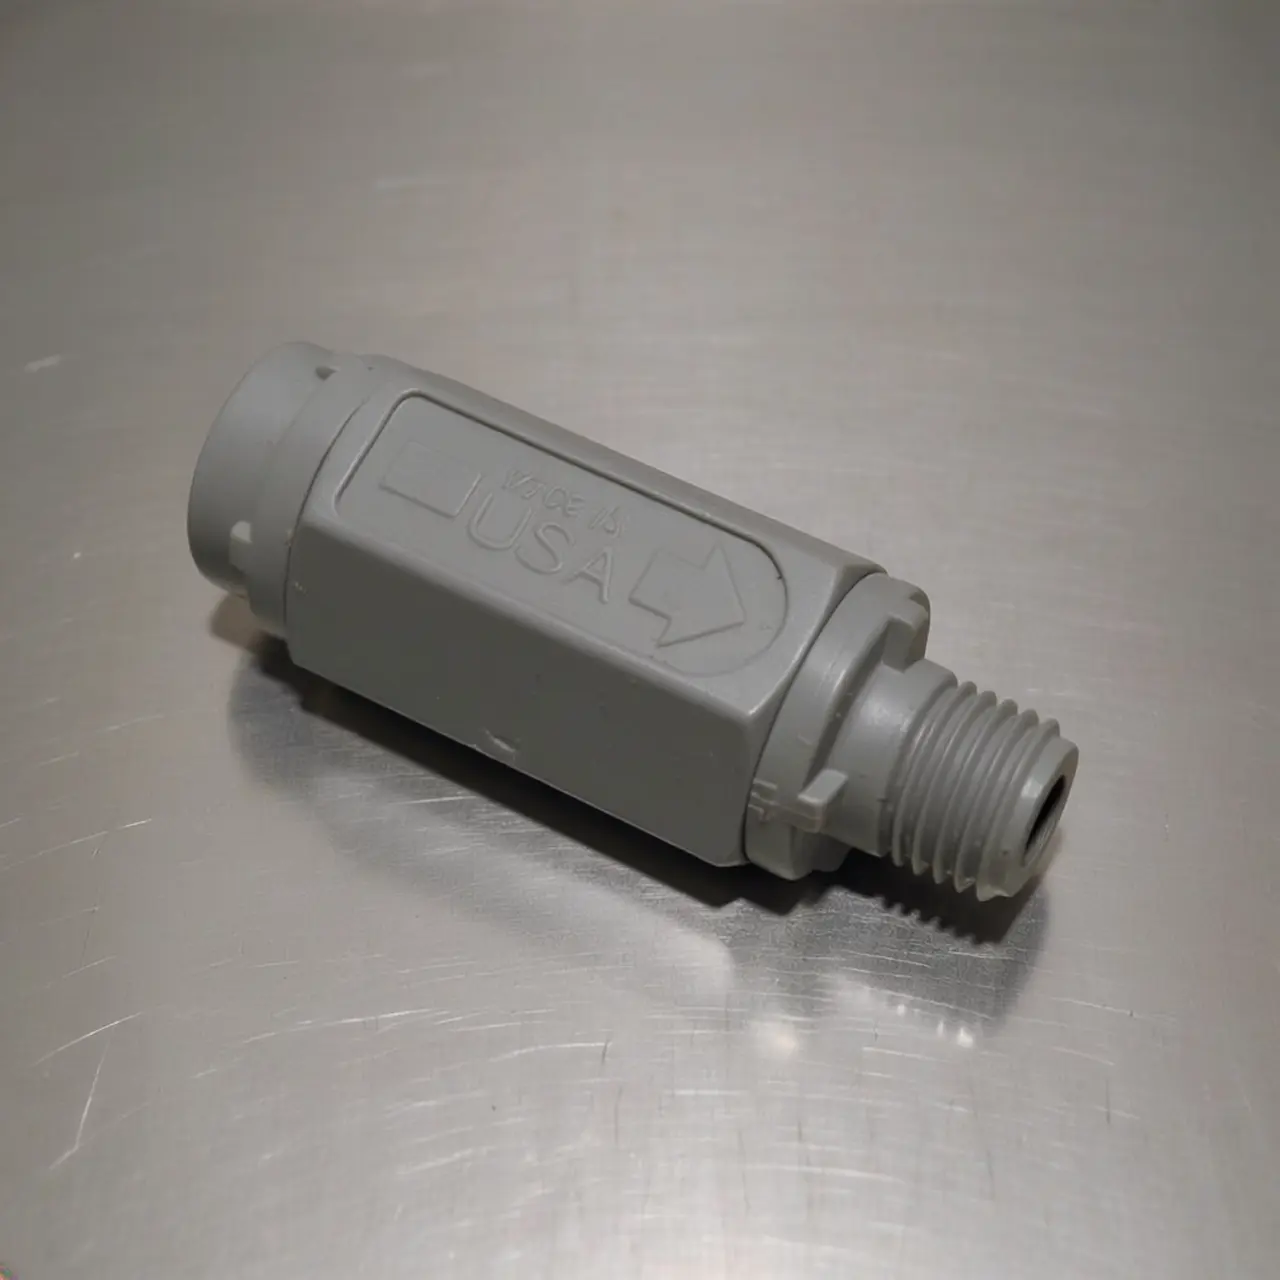
Non-Return Valve for Technifoamer is a practical choice for everyday workplace requirements.
Available in 4 pack sizes
Suresan is a high-performance broad spectrum sanitiser formulated for use across the food, dairy, and beverage industries.
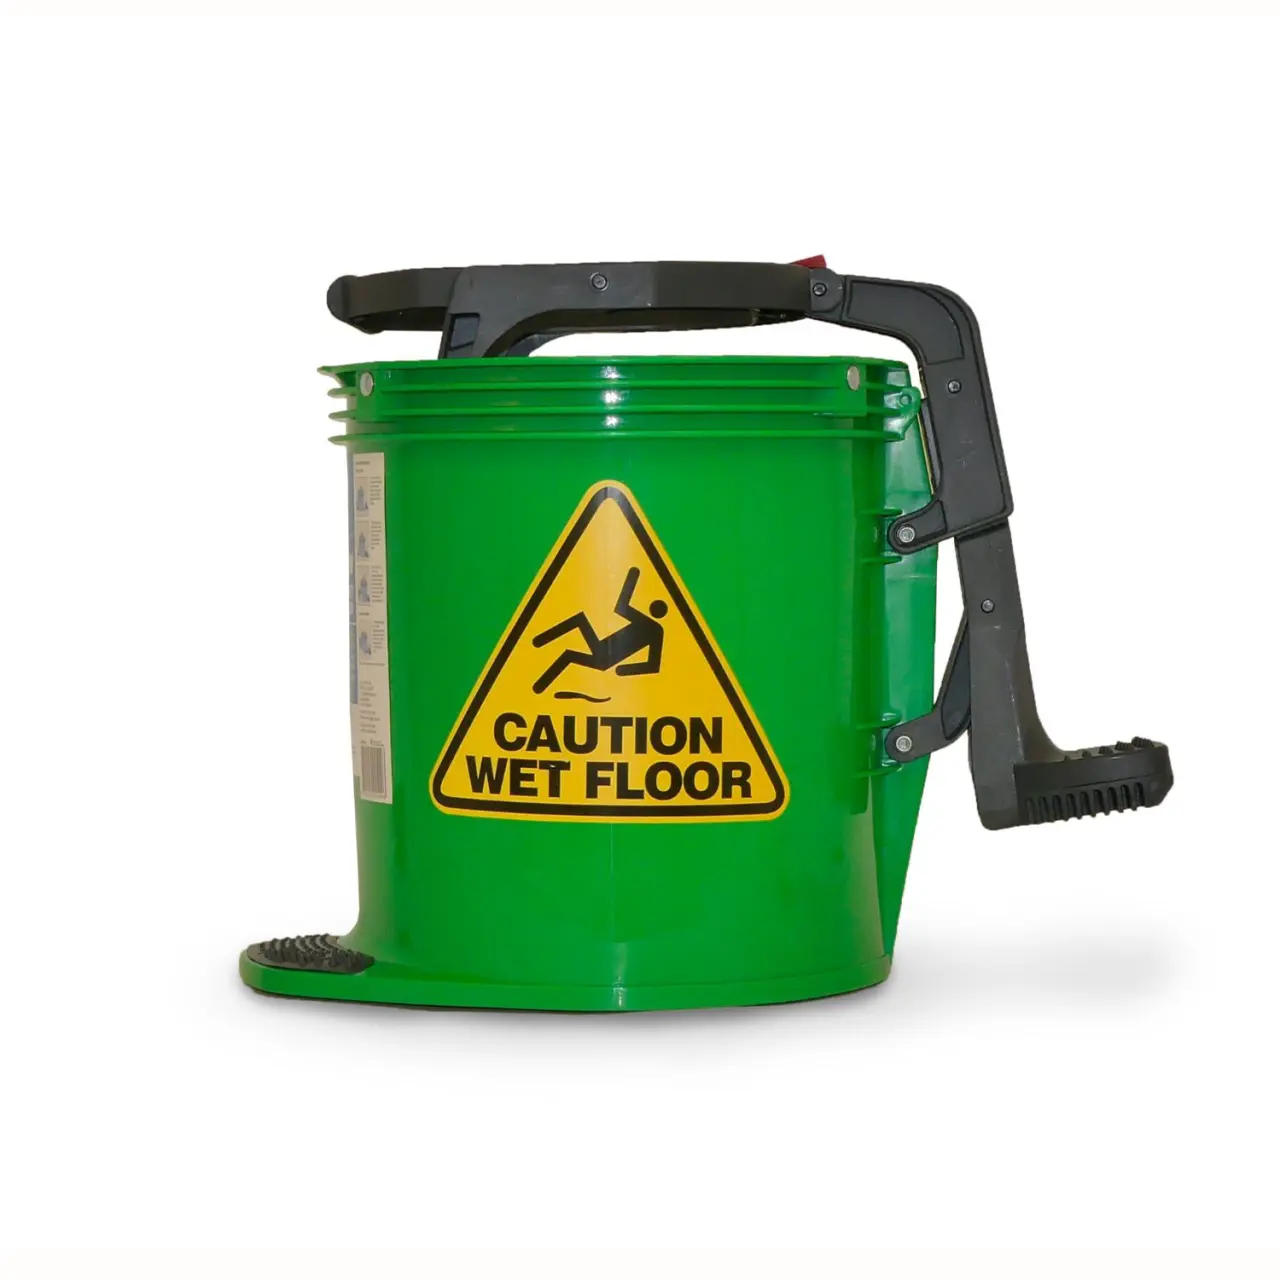
Available in 9 colours
Designed for dependable performance in professional wringer buckets applications.
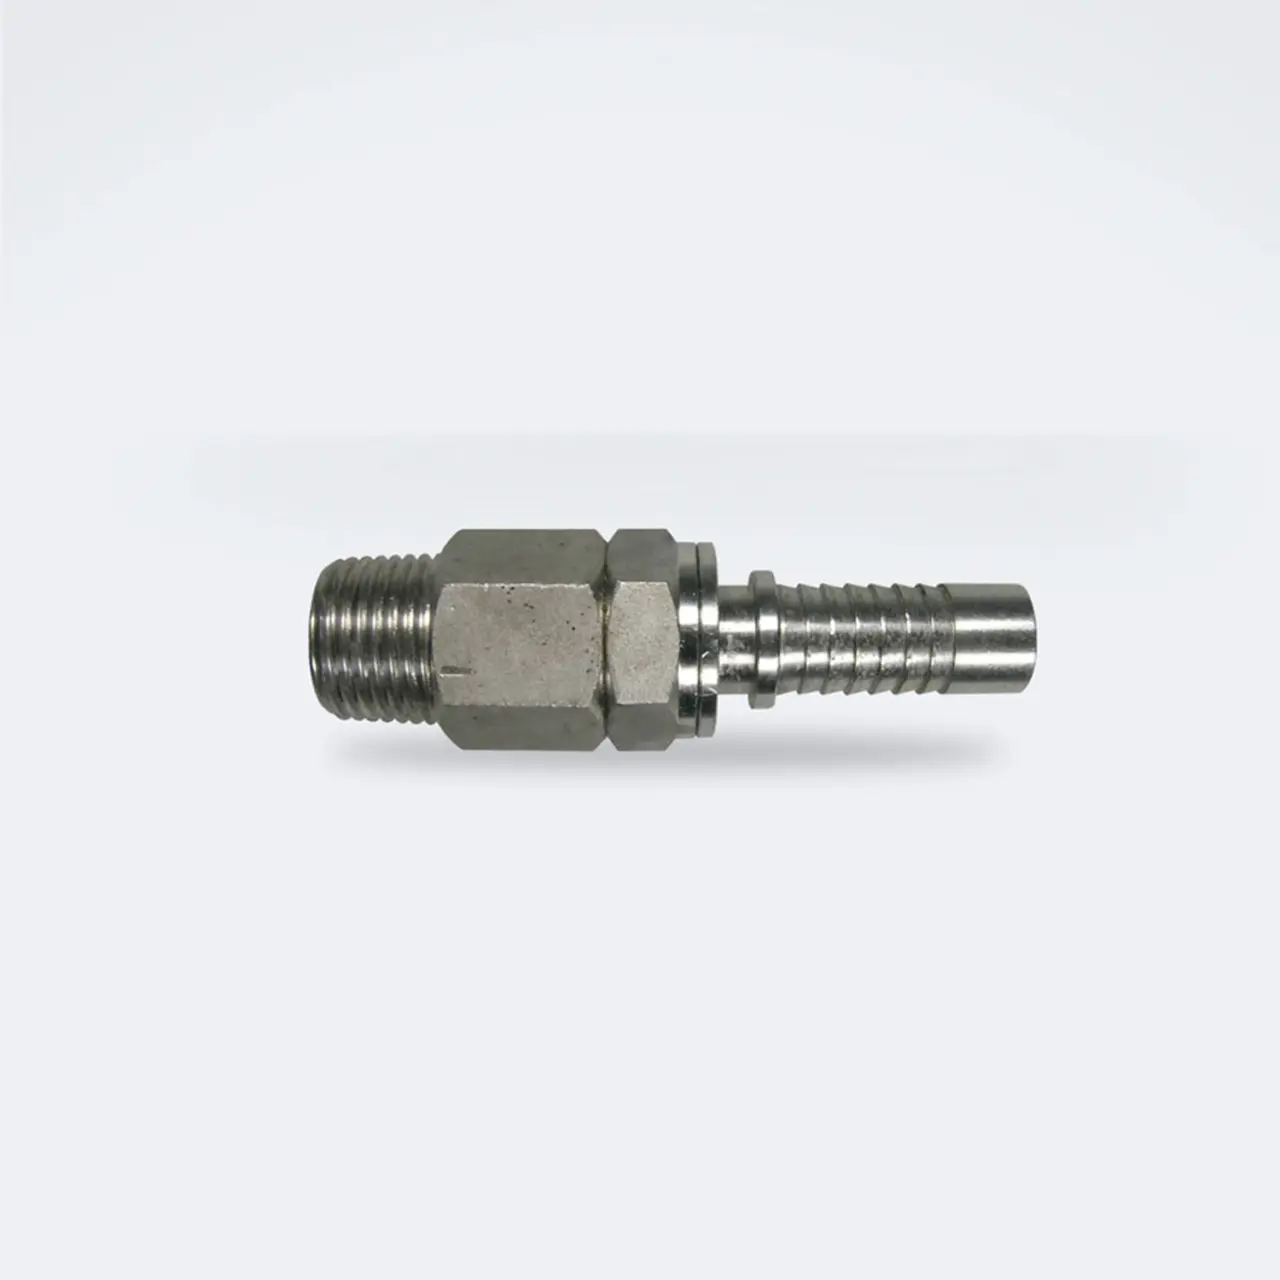
The swivelling hose tail can be used for a swivelling connection between a flexible hose and a spray gun for more comfort.
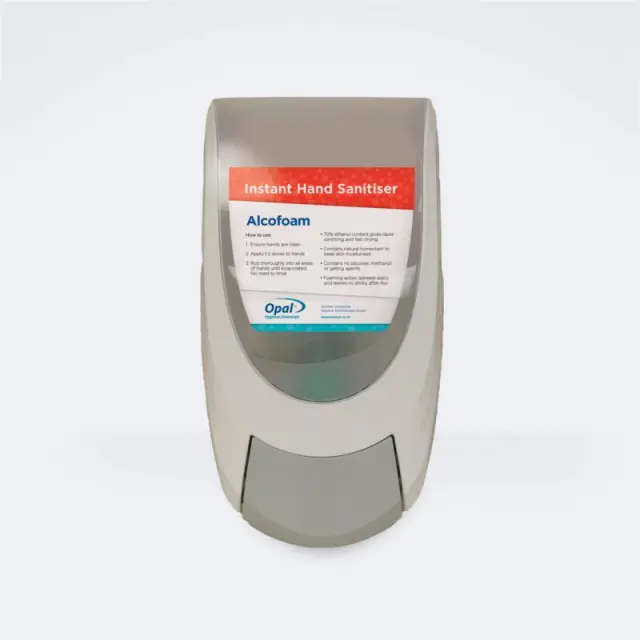
Wall mounted stylish dispenser, lockable. Quality design ensures long trouble-free service life.
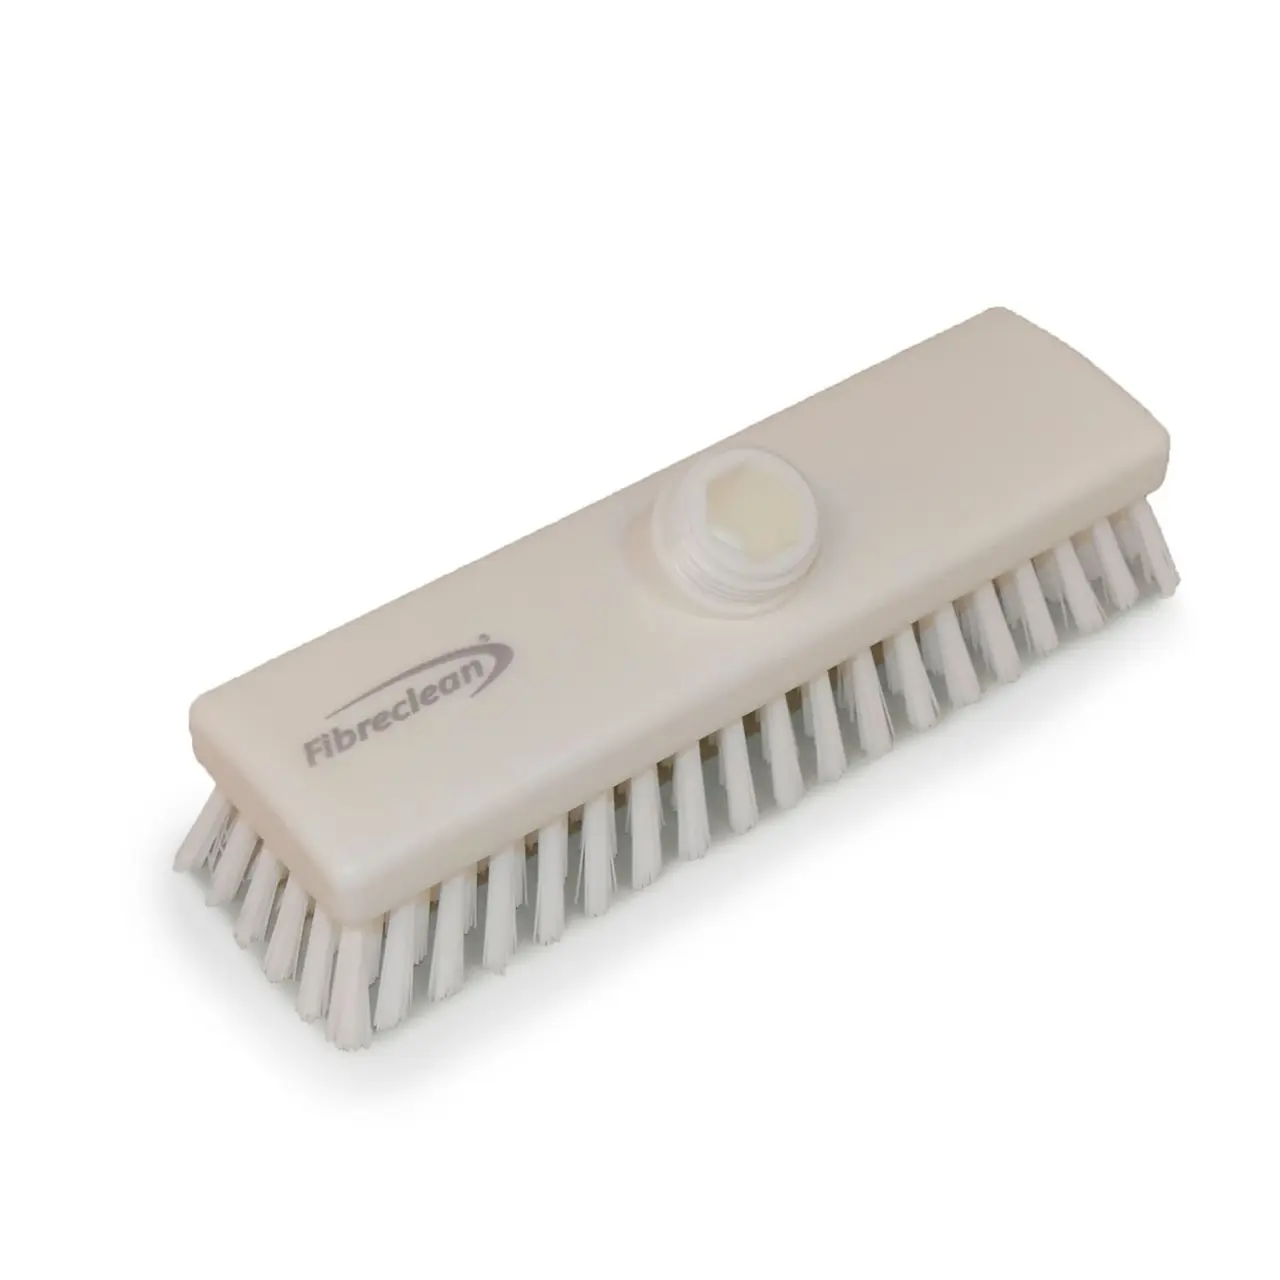
Available in 5 sizes, 3 bristles and 9 colours
As with all Deck Scrubs, these have short, stiff bristles to scrub and loosen debris on the floor.
Talk to a hygiene specialist. We'll help you build the right system for your site: tools, chemicals, visual management and all.